Spark Detection & Extinguishing Systems
Safety in Milliseconds
During production, sparks or glowing embers can easily be produced by the processing machines themselves or from impurities in the conveyed material. These potential ignition sources are then taken up by the pneumatic system and carried along with highly flammable chips, dust or other finely divided particles. A single spark entering the filters, silos or dust collector is enough to cause fires or dust explosions, resulting in extreme property damage and costly downtime, or worse, life threatening.
A potential disaster of this magnitude is best handled with immediate, effective and reliable preventative measures. With Teza, VdS and FM approved systems, sparks are detected and extinguished before they reach the filter or dust collector, thus protecting all company assets. The protection strategy is in the installation of these systems, which has been successfully tried and tested in thousands of applications around the world; Teza has the necessary infrastructure and is in an expert position.
Fire Protection for Chip Silos
Silo fires are often caused by hot parts (A) from the incineration plant entering the silo.
- Leaks in the rotary gate valve upstream of the furnace.
- The oven is not fed continuously.
- Drawing embers out of the furnace with the silo acting as a chimney.
- Hot gases in the silo can cause combustion.
By installing a spark detection system (B) with extinguishing device (C), these fire hazards can be effectively combated. In addition, all pneumatic supply lines and return air ducts must be monitored for flying sparks.
Fire or explosion can occur wherever flammable materials are transported by mechanical or pneumatic means. Automatic electronic spark extinguishing systems can be used effectively here.
Examples of areas where spark extinguishing systems are used
- Bitumen processing
- Battery production
- Cotton wool industry
- Chemical industry
- Incineration plants
- Rubber industry
- Industrial ovens
- Wood industry
- Coffee roasting machines
- Coal dust extraction plants
- Synthetic materials industry
- Food industry
- Leather industry
- Metal processing industry
- Milk powder drying
- Waste incineration plants
- Paper mills
- Recycling industry
- Tire industry
- Chipboard factories
- Textile industry
Working Principle
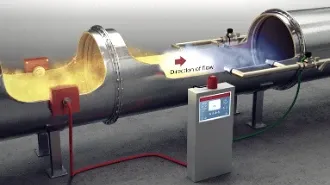
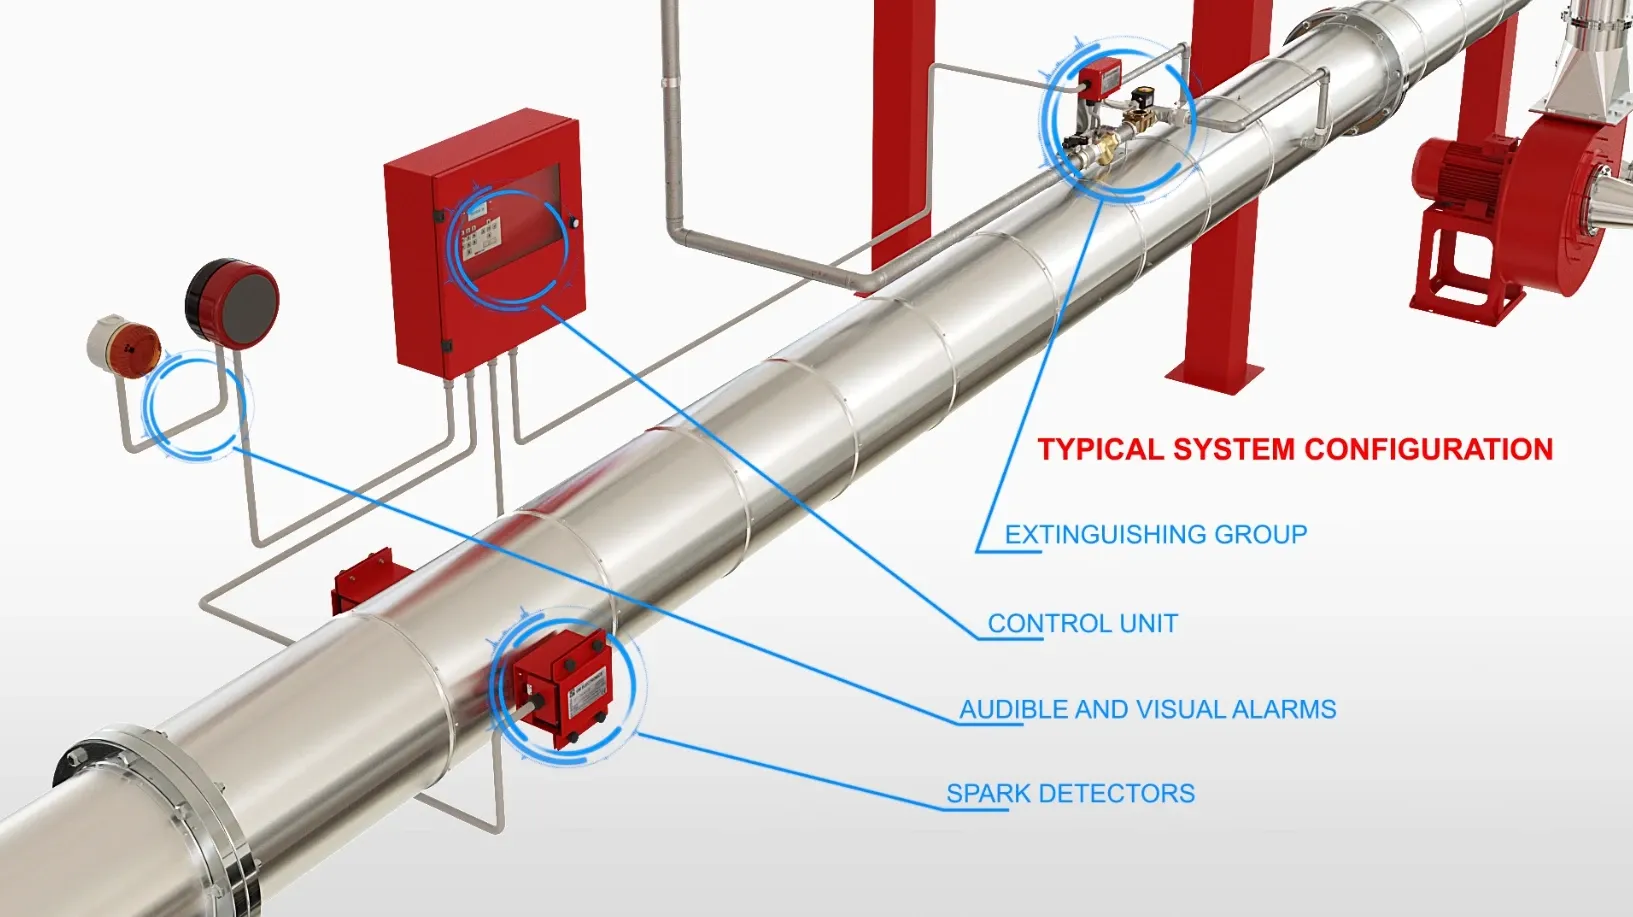
Spark extinguishing system consists of control panel, spark detectors and automatic extinguishing unit. Sparks passing through the channels of the conveying system are instantly detected by infrared spark detectors flush-mounted on the outer surface of the duct. The spark detector sends a signal to the control panel, which triggers the automatic extinguishing unit’s solenoid valve while simultaneously activating an audible alarm. The extinguishing water is discharged in milliseconds and is discharged into the channel by specially placed patented flat spray nozzles creating a circular water wall inside the pipe. The glowing particles go to the water spray curtain. Immediately after, the solenoid valve closes automatically. The full detection and extinguishing process normally runs during production to eliminate expensive downtime. Depending on the amount of potential ignition sources, automatic shutdown of the conveying (conveyor) machine is also possible.
Highlights
It detects the first ignition in suction and transport systems and creates a water curtain instantly with its automatic extinguishing feature to suffocate the smoldering particles. These systems are recommended for use in areas where flammable materials are transported pneumatically and where there is a high risk of fire or dust explosion due to sparks or smoldering particles. As a rule, the extinguishing process takes place without interrupting operations.
Application
- Dust Extraction Filtration & Silos
- Conveyor Systems
- Pneumatic Suction Points
- Powder Coating and Ovens
Advantages
- Flexible Design & Easy Installation
- Monitoring of Faults
- Wide Nozzle Protection Area
- No Downtime in the Process
System Applications
Spark detection-extinguishing systems, which can be customized and applied in accordance with the equipment of the enterprises, have a wide application area. Attention should be paid to the fact that spark extinguishing systems detectors are tested and certified at the point where they provide protection together with extinguishing apparatus and other accessories.
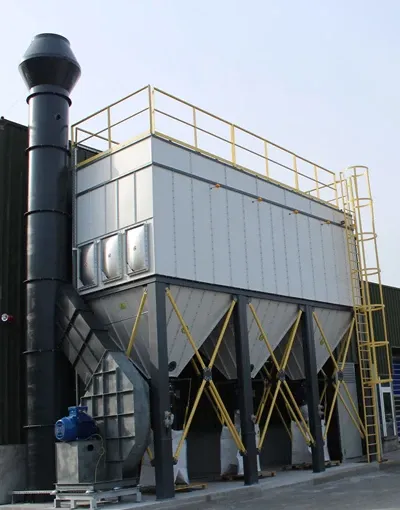
Dust Extraction Filters 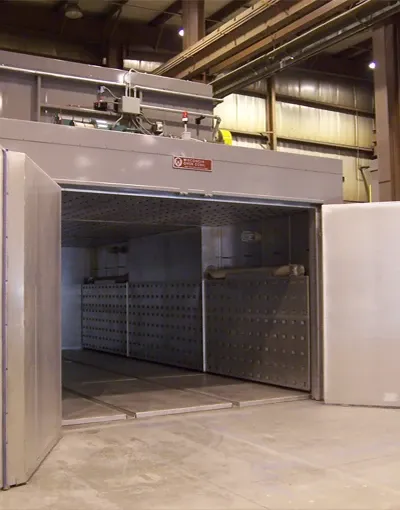
Industrial OvensPowder Coating Units 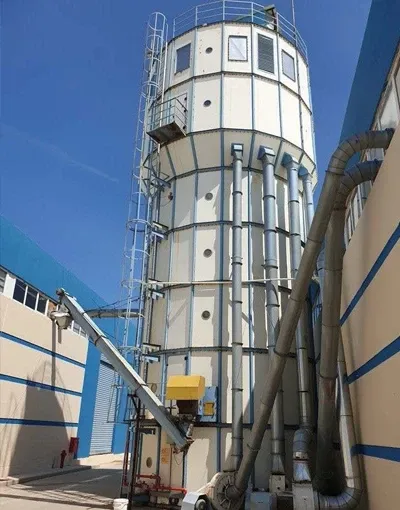
Dust Extraction Silos
Related Solutions
Let's Identify the Risks in Your Process
Let's determine together what precautions should be taken regarding explosion and fire safety in your facility.
